Weld Overlay vs Explosion Bonding vs Roll Bonding vs ESSC Strip Cladding vs Hot Rolling Cladding Methods Comparison Matrix: Corrosion-Resistant Alloy Cladding Method Selection for Refinery, Petrochemical, and Chemical Pressure Vessel Fabrication

Weld Overlay vs Explosion Bonding vs Roll Bonding vs ESSC Strip Cladding vs Hot Rolling Cladding Methods Comparison Matrix: Corrosion-Resistant Alloy Cladding Method Selection for Refinery, Petrochemical, and Chemical Pressure Vessel Fabrication

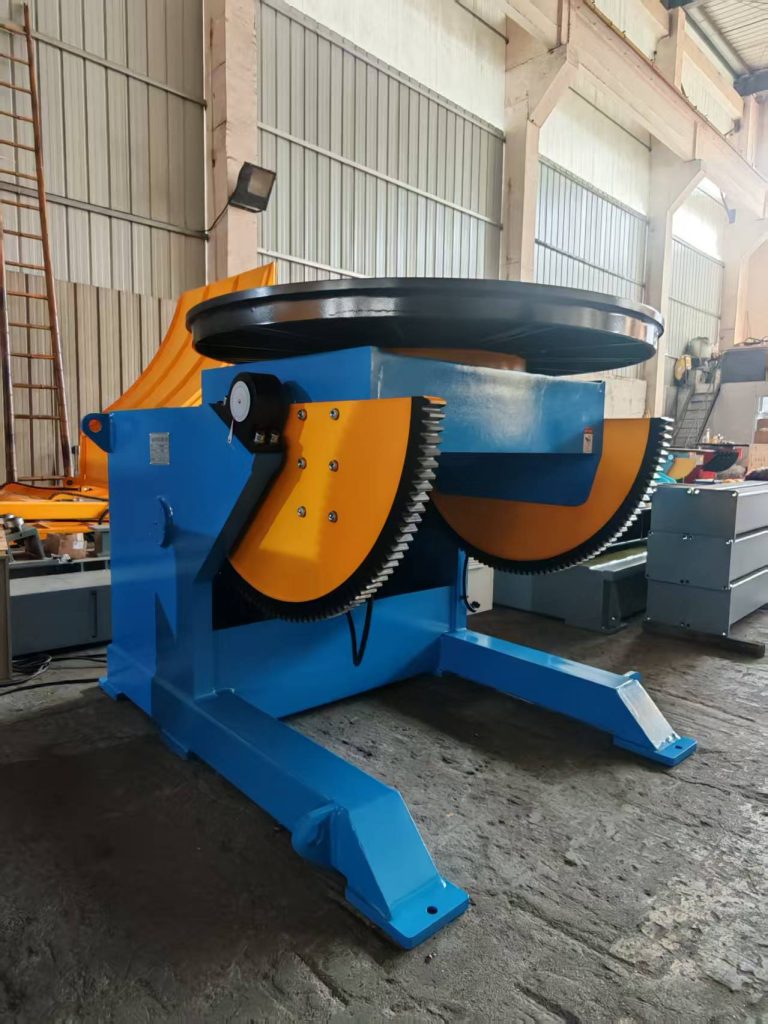
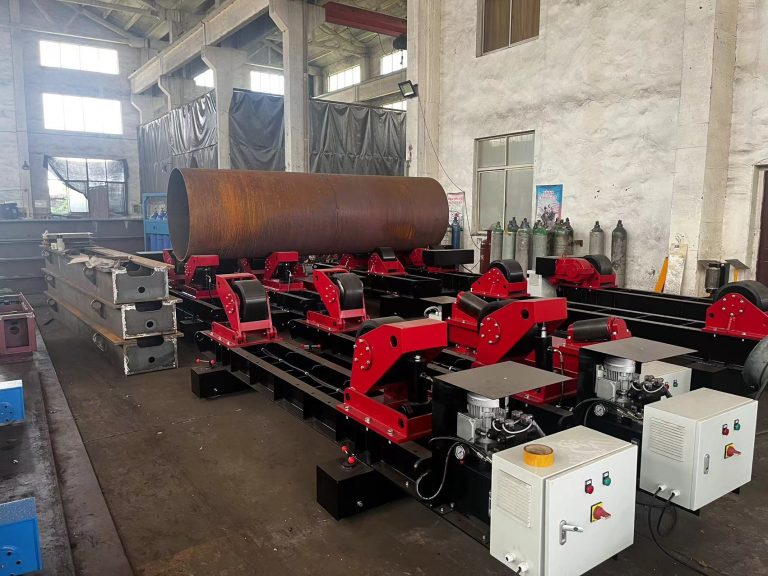
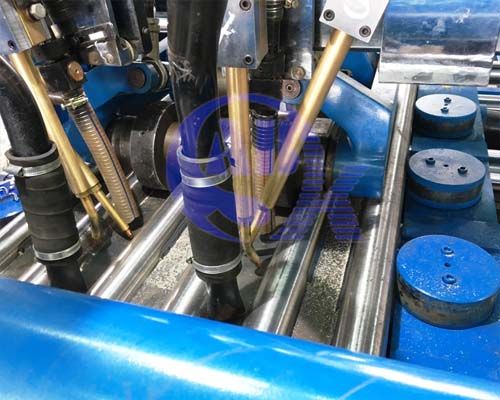
This matrix compares weld overlay, ESSC strip cladding, explosion bonding, roll bonding and hot rolling cladding on deposition rate, thickness, dilution, bond quality and cost per m² for refinery and chemical pressure vessels. Wuxi ABK Cell A and HGZ/LH equipment support single-electrode overlay, ESSC integration and clad-plate fabrication.
ASME BPVC Section I (Power Boiler) vs Section III (Nuclear Component) vs Section VIII (Pressure Vessel) Code Cross-Family Comparison Matrix: Fabricator Selection, Certification Investment, and Application Boundary Guide for Boiler, Reactor, and Pressure Vessel Manufacturers

ASME BPVC Section I (Power Boiler) vs Section III (Nuclear Component) vs Section VIII (Pressure Vessel) Code Cross-Family Comparison Matrix: Fabricator Selection, Certification Investment, and Application Boundary Guide for Boiler, Reactor, and Pressure Vessel Manufacturers

This matrix compares ASME Section I, Section III, and Section VIII across scope, design method, stamps, and certification cost. It also clarifies application boundaries among boilers, nuclear components, and pressure vessels, with fabricator landscape and Wuxi ABK equipment support.

ASME Section VIII Division 2 Alternative Rules for Pressure Vessel Construction: Design-by-Analysis Reference for High-Integrity Refinery, Petrochemical, and Nuclear Pressure Vessel Fabricators

ASME Section VIII Division 2 Alternative Rules for Pressure Vessel Construction: Design-by-Analysis Reference for High-Integrity Refinery, Petrochemical, and Nuclear Pressure Vessel Fabricators

ASME Section VIII Division 2 is the design-by-analysis alternative to Div 1, using detailed stress/fatigue/fracture analysis and tighter documentation to support ASME U2-stamp pressure vessels with 15–30% wall-thickness reduction for refinery, petrochemical, LNG, aerospace and SMR applications. Wuxi ABK welding automation—HGZ rotators, manipulators, positioners and digital-twin/machine-vision QA with calibrated parameter logging—supports Div 2 welding quality, 100% NDE, PWHT/toughness and U2-stamp documentation chains.

ASME B16.9 Factory-Made Wrought Butt-Welding Fittings: Elbow, Tee, Reducer, Cap, and Cross Reference for Pressure Vessel Nozzle + Process Piping + Pipeline Spool Fabrication

ASME B16.9 Factory-Made Wrought Butt-Welding Fittings: Elbow, Tee, Reducer, Cap, and Cross Reference for Pressure Vessel Nozzle + Process Piping + Pipeline Spool Fabrication

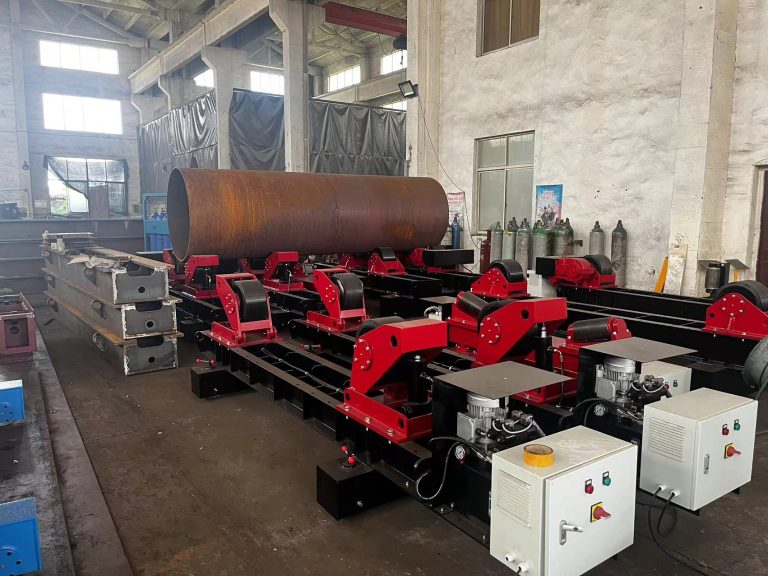
ASME B16.9 is the dimensional and pressure-temperature rating standard for factory-made wrought butt-welding fittings including elbow, tee, reducer, cap, and cross. This guide covers material specifications, welding considerations, and Wuxi ABK equipment (HBJ positioner, HGZ rotator, ZHGK fit-up, TTW orbital) for pressure vessel nozzle, process piping, and pipeline spool fabrication.

Pemamek vs Wuxi ABK Welding Equipment: A Procurement Manager’s Guide for Wind Tower and Heavy Pressure Vessel Projects

Pemamek vs Wuxi ABK Welding Equipment: A Procurement Manager’s Guide for Wind Tower and Heavy Pressure Vessel Projects

A procurement manager’s walkthrough comparing Pemamek and Wuxi ABK welding equipment across capacity, lead time, cost, customization, service coverage, and wind-tower-specific capability — with a clear decision pattern for 2026 wind tower and heavy pressure vessel fabrication projects.