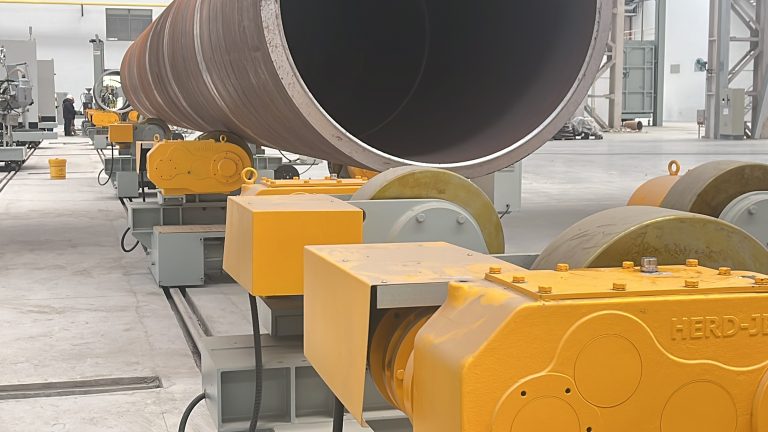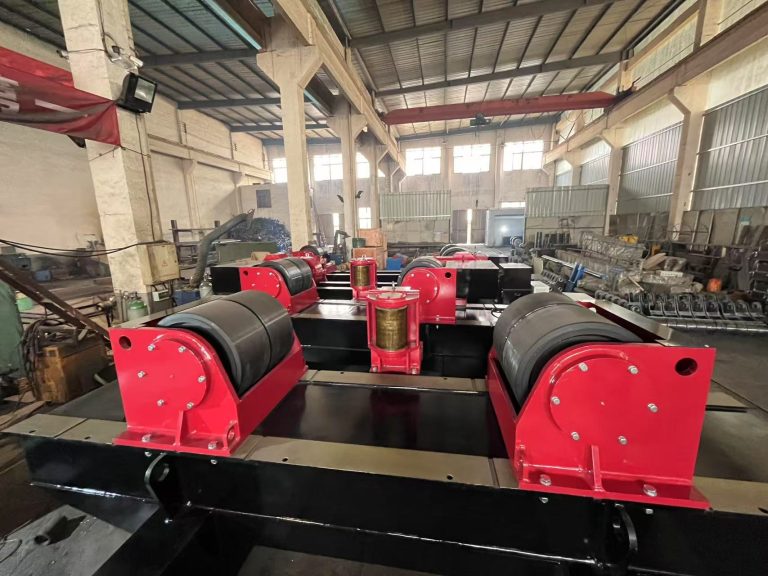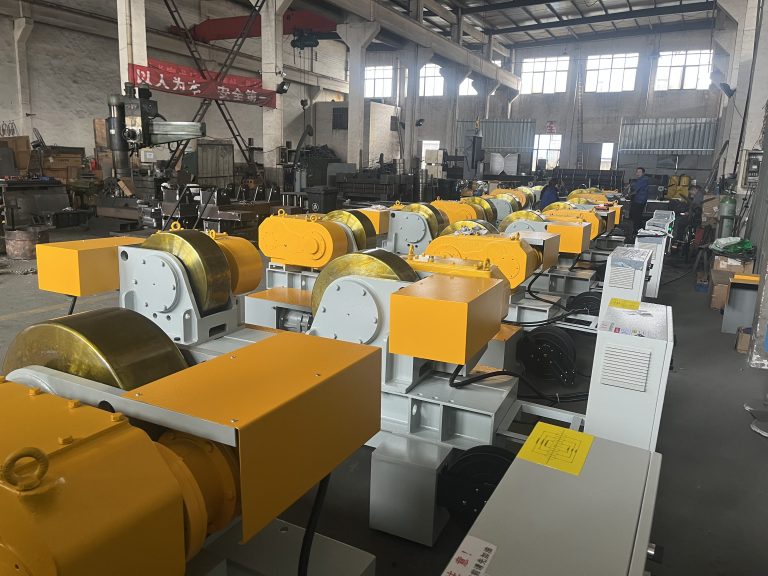
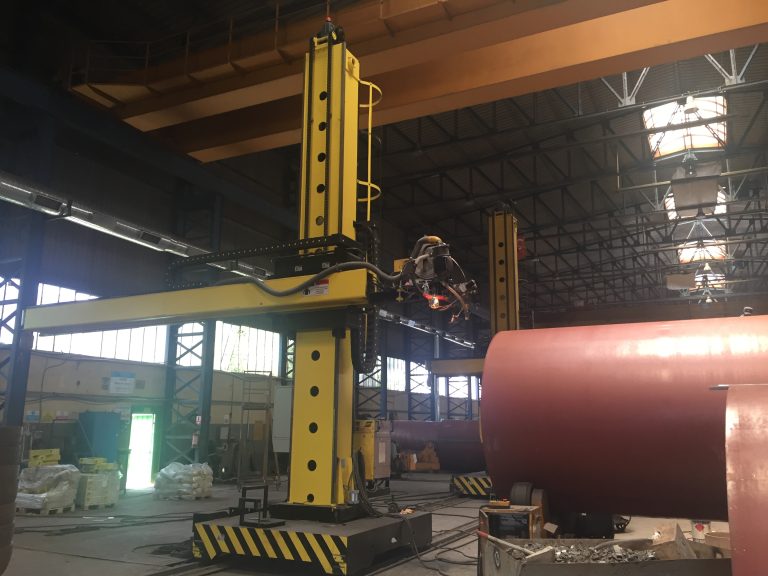
ASME Section VIII Division 1 vs Division 2 vs Division 3 for 350 bar, 700 bar, and 1000 bar Hydrogen Storage Vessel: Design Margin, Wall Thickness, Welding Requirement, and Fabrication Cost Comparison Matrix for Hydrogen Refueling Station and Industrial Hydrogen Storage Fabricators

ASME Section VIII Division 1 vs Division 2 vs Division 3 for 350 bar, 700 bar, and 1000 bar Hydrogen Storage Vessel: Design Margin, Wall Thickness, Welding Requirement, and Fabrication Cost Comparison Matrix for Hydrogen Refueling Station and Industrial Hydrogen Storage Fabricators

Comparative decision guide on ASME Section VIII Div 1 vs Div 2 vs Div 3 for 350, 700, and 1000 bar hydrogen storage vessels. Covers wall thickness, welding requirements, fabrication costs, and Wuxi ABK automation equipment fit for H2 refueling stations.
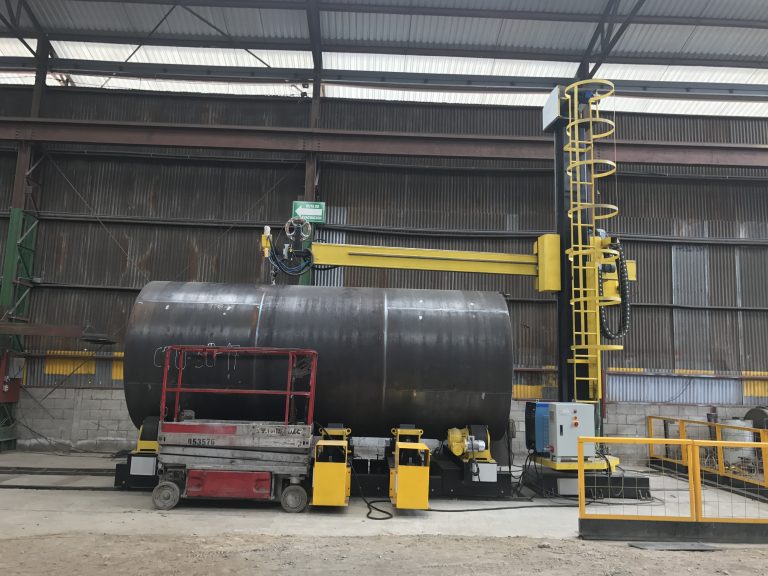
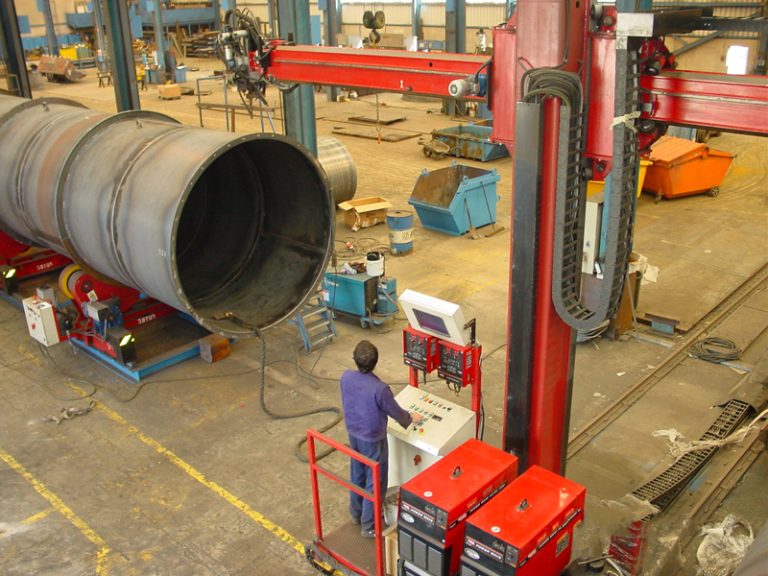
ASME B96.1 + API 620 Appendix AL + AA (Aluminum Association) + AWS D1.2 Aluminum Welded Storage Tank and Structural Standards: Design + Fabrication Reference for Aluminum Cryogenic, Chemical, Marine, and Aerospace Fabricators

ASME B96.1 + API 620 Appendix AL + AA (Aluminum Association) + AWS D1.2 Aluminum Welded Storage Tank and Structural Standards: Design + Fabrication Reference for Aluminum Cryogenic, Chemical, Marine, and Aerospace Fabricators

Navigate the ASME B96.1, API 620 Appendix AL & AWS D1.2 aluminum welding standard family. Wuxi ABK supports fabricators with automation equipment for marine, tank & aerospace projects.

ASME NM.1 + NM.2 + NM.3 + ISO 15494 + DVS 2207 Thermoplastic and Non-Metallic Piping System Standards: Design + Fusion Joining Reference for Chemical Processing, Water Treatment, Semiconductor, and Pharmaceutical Non-Metallic Fluid System Fabricators

ASME NM.1 + NM.2 + NM.3 + ISO 15494 + DVS 2207 Thermoplastic and Non-Metallic Piping System Standards: Design + Fusion Joining Reference for Chemical Processing, Water Treatment, Semiconductor, and Pharmaceutical Non-Metallic Fluid System Fabricators

ASME NM.1 + ISO 15494 + DVS 2207 non-metallic piping design & fusion joining reference for chemical, semiconductor & pharma. Wuxi ABK supports hybrid metal-thermoplastic systems.

ASME Section VIII Division 3 for High-Pressure Vessel Construction: Design + Fabrication Reference for Ultra-High-Pressure Hydrogen Storage, Hydraulic Accumulator, Isostatic Press, and Autoclave Fabricators

ASME Section VIII Division 3 for High-Pressure Vessel Construction: Design + Fabrication Reference for Ultra-High-Pressure Hydrogen Storage, Hydraulic Accumulator, Isostatic Press, and Autoclave Fabricators

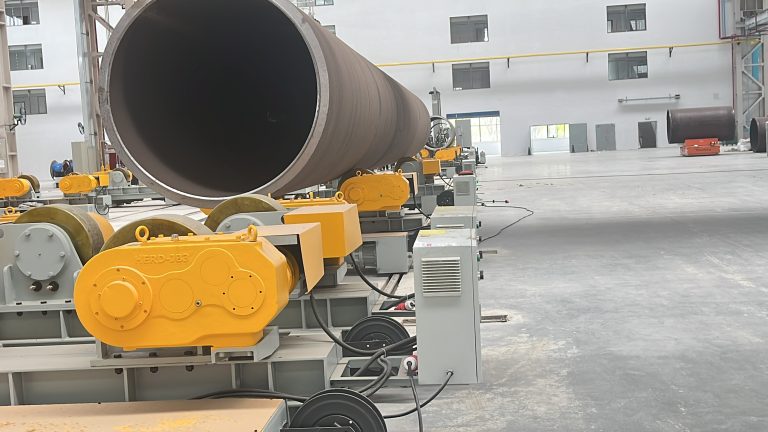
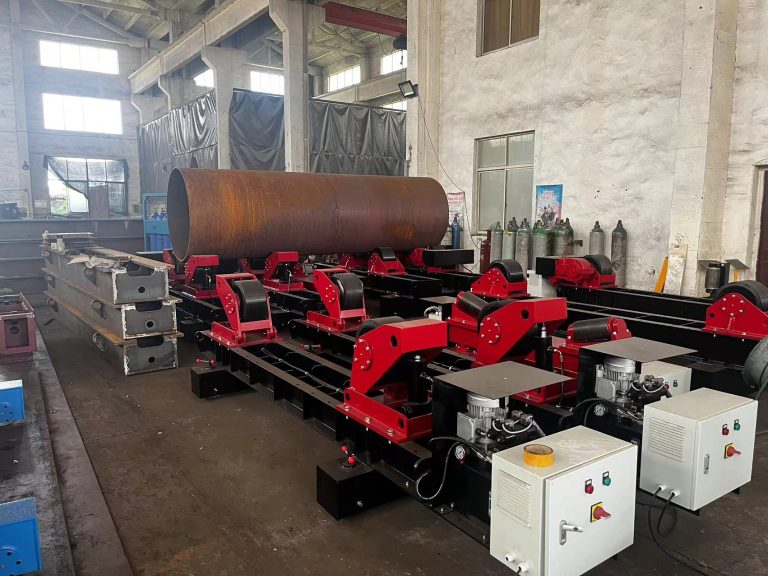
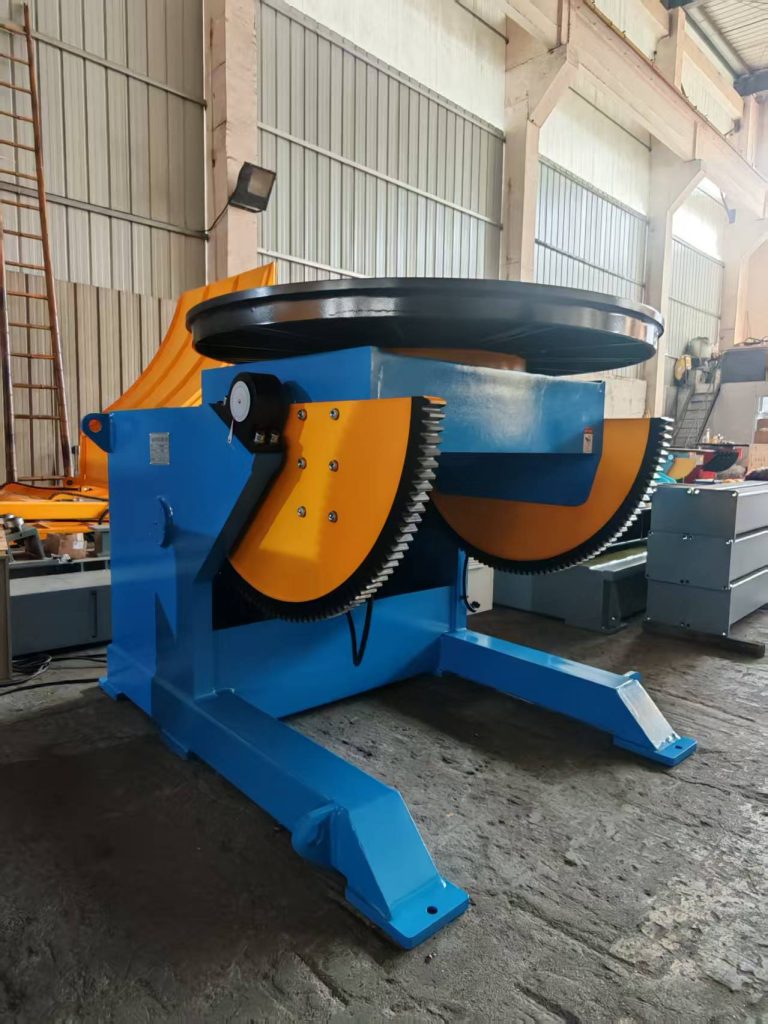
Wuxi ABK hydraulic welding rotator and welding automation equipment for heavy-duty vessel fabrication, supporting ASME Section VIII Division 3 / U3-stamp high-pressure vessel and hydrogen storage weld workflows.

ASME Section VIII Division 2 Alternative Rules for Pressure Vessel Construction: Design-by-Analysis Reference for High-Integrity Refinery, Petrochemical, and Nuclear Pressure Vessel Fabricators

ASME Section VIII Division 2 Alternative Rules for Pressure Vessel Construction: Design-by-Analysis Reference for High-Integrity Refinery, Petrochemical, and Nuclear Pressure Vessel Fabricators

ASME Section VIII Division 2 is the design-by-analysis alternative to Div 1, using detailed stress/fatigue/fracture analysis and tighter documentation to support ASME U2-stamp pressure vessels with 15–30% wall-thickness reduction for refinery, petrochemical, LNG, aerospace and SMR applications. Wuxi ABK welding automation—HGZ rotators, manipulators, positioners and digital-twin/machine-vision QA with calibrated parameter logging—supports Div 2 welding quality, 100% NDE, PWHT/toughness and U2-stamp documentation chains.

ASME B16.34 Valves — Flanged, Threaded, and Welding End: Pressure-Temperature Rating and Weld End Fabrication Reference for Pressure Vessel and Process Piping Valve Suppliers

ASME B16.34 Valves — Flanged, Threaded, and Welding End: Pressure-Temperature Rating and Weld End Fabrication Reference for Pressure Vessel and Process Piping Valve Suppliers

Guide to ASME B16.34 valve welding integration. Wuxi ABK Machinery supplies welding rotators, positioners, and manipulators for valve-to-pipe spool fabrication.

ASME B16.9 Factory-Made Wrought Butt-Welding Fittings: Elbow, Tee, Reducer, Cap, and Cross Reference for Pressure Vessel Nozzle + Process Piping + Pipeline Spool Fabrication

ASME B16.9 Factory-Made Wrought Butt-Welding Fittings: Elbow, Tee, Reducer, Cap, and Cross Reference for Pressure Vessel Nozzle + Process Piping + Pipeline Spool Fabrication

ASME B16.9 is the dimensional and pressure-temperature rating standard for factory-made wrought butt-welding fittings including elbow, tee, reducer, cap, and cross. This guide covers material specifications, welding considerations, and Wuxi ABK equipment (HBJ positioner, HGZ rotator, ZHGK fit-up, TTW orbital) for pressure vessel nozzle, process piping, and pipeline spool fabrication.

ASME B31.9 Building Services Piping: Welding Reference for Commercial Building, Hospital, Data Center, Semiconductor Fab, and Institutional HVAC + Steam + Chilled Water Piping

ASME B36.10 + B36.19 govern pipe OD, wall thickness, and NPS designation for carbon and stainless steel pipe spool fabrication. Learn 5 common procurement mistakes and Wuxi ABK equipment support.

ASME B36.10 + B36.19 Pipe Dimensions Standards: Nominal Pipe Size, Schedule, and Wall Thickness Reference for Carbon Steel and Stainless Steel Pipe Spool Fabrication

ASME B36.10 + B36.19 govern pipe OD, wall thickness, and NPS designation for carbon and stainless steel pipe spool fabrication. Learn 5 common procurement mistakes and Wuxi ABK equipment support.

ASME B31.8 Gas Transmission and Distribution Piping Systems: Class Location-Based Welding Reference for Natural Gas, Fuel Gas, and Gas Storage Pipeline Contractors

ASME B31.8 governs cross-country natural gas, fuel gas, and LNG facility piping with unique Class Location design factors (F 0.80 to 0.40). Learn 5 B31.8 project scenarios and Wuxi ABK equipment support.

ASME B31.4 Pipeline Transportation Systems for Liquid Hydrocarbons, Anhydrous Ammonia, CO₂, and Slurries: Cross-Country Liquid Pipeline Welding Reference for Oil, Petrochemical, and CCUS Pipeline Contractors

ASME B31.4 governs cross-country liquid pipeline construction for crude oil, refined products, LPG, anhydrous ammonia, CO₂, and slurries. Learn 5 B31.4 project scenarios and Wuxi ABK equipment support.

DNV-ST-F101 Submarine Pipeline Welding Fabrication Line: Documentation Chain for Offshore Pipeline Spool, Tie-In, and Subsea Fabricators

DNV-ST-F101 Submarine Pipeline Welding Fabrication Line: Documentation Chain for Offshore Pipeline Spool, Tie-In, and Subsea Fabricators

DNV-ST-F101 submarine pipeline projects require traceable welding, fit-up control, NDE-ready weld geometry, coating handling, and repair loop discipline. 6 documentation areas + offshore pipeline equipment stack + 5 project scenarios + DNV-ST-F101 vs API 1104 comparison.

ASME B31.12 Hydrogen Piping and Pipelines: H₂ Service Welding Requirements for Hydrogen Economy, Green Steel, and Power-to-X Project Fabricators

ASME B31.12 Hydrogen Piping and Pipelines: H₂ Service Welding Requirements for Hydrogen Economy, Green Steel, and Power-to-X Project Fabricators

ASME B31.12 (Hydrogen Piping and Pipelines) governs piping in hydrogen service across hydrogen economy + green steel + Power-to-X applications — covering Part GR (general), Part IP (industrial piping), Part PL (pipeline). Hydrogen embrittlement screening drives material from carbon steel (HV ≤235 HAZ) → austenitic stainless → SA-372 Class IV/V → Inconel. 5 welding requirements (WPS Sec IX+B31.12 Appendix / low-H consumable ≤4 mL/100g / hardness HV ≤235 / PWHT mandatory CS+low-alloy / 100% NDE + helium leak high-pressure). 5 project scenarios + B31.12 vs B31.3 vs API 1104 comparison.

ASME B31.1 Power Piping: Boiler External Piping, Main Steam, and Hot Reheat Piping Welding Reference for Utility Boiler and Combined Cycle Plant Fabricators

ASME B31.1 Power Piping: Boiler External Piping, Main Steam, and Hot Reheat Piping Welding Reference for Utility Boiler and Combined Cycle Plant Fabricators

ASME B31.1 Power Piping governs piping in steam power generating stations, utility boilers, combined cycle plants, cogeneration — Boiler External Piping (BEP per Section I I-stamp), main steam + hot reheat + cold reheat + feedwater + balance-of-plant. Material SA-106 Gr B carbon to SA-335 P11/P22/P91 Cr-Mo supercritical 565-625°C. 5 welding requirements (WPS Section IX / mandatory PWHT Cr-Mo / Charpy / 100% RT BEP+main steam / 1.5× hydrotest). 5 project scenarios + B31.1 vs B31.3 comparison.

ASME B16.5 Pipe Flange and Flanged Fittings: Class 150 / 300 / 600 / 900 / 1500 / 2500 Pressure-Temperature Ratings and Flange Welding for Pressure Vessel Connections

ASME B16.5 Pipe Flange and Flanged Fittings: Class 150 / 300 / 600 / 900 / 1500 / 2500 Pressure-Temperature Ratings and Flange Welding for Pressure Vessel Connections

ASME B16.5 governs pipe flange and flanged fittings (NPS 1/2 through 24) — 7 Class ratings (150-2500) × 5 face types (RF / FF / RTJ / T&G / Lap Joint) × multiple material groups (Group 1.1 carbon to Group 3 nickel alloy). 5 flange welding configurations (WN / SO / Socket Weld / Threaded / Blind) + Section IX WPS qualification + SFA-5 consumable selection + UCS-56 PWHT requirements + 5 procurement mistakes. Real Project hydrocracker Class 1500 RTJ + SA-182 F22.

ASME Section II Part C SFA-5 Welding Consumables Specification: SFA-5.1 SMAW / SFA-5.5 Low-Alloy / SFA-5.18 GMAW / SFA-5.20 FCAW Procurement Guide for Pressure Vessel Fabricators

ASME Section II Part C SFA-5 Welding Consumables Specification: SFA-5.1 SMAW / SFA-5.5 Low-Alloy / SFA-5.18 GMAW / SFA-5.20 FCAW Procurement Guide for Pressure Vessel Fabricators

ASME Section II Part C SFA-5 welding consumables specification governs electrode, filler metal, and flux for pressure vessel + boiler fabrication. 6 critical SFA-5 specifications (5.1 SMAW carbon / 5.5 SMAW low-alloy / 5.17 SAW carbon / 5.18 GMAW / 5.20 FCAW / 5.23 SAW Cr-Mo) + 5-position classification system + base-material selection quick reference (SA-516 / SA-387 / SA-203 / SA-353 / SA-240 / S31803) + 7-step procurement decision framework + 5 common mistakes.

ASME Section VIII Division 1 UG-84 Charpy V-Notch Impact Testing: Test Specimen Preparation, Test Temperature, and Acceptance Criteria for Pressure Vessel Welding

ASME Section VIII Division 1 UG-84 Charpy V-Notch Impact Testing: Test Specimen Preparation, Test Temperature, and Acceptance Criteria for Pressure Vessel Welding

ASME Section VIII Division 1 UG-84 prescribes Charpy V-notch impact testing methodology for pressure vessel base metal, weld metal, and HAZ. 5 specification areas (specimen geometry / orientation / quantity / temperature / acceptance) + 4 notch locations (base + weld center + HAZ 1mm + HAZ 5mm) + 5-criterion acceptance + bath medium selection by MDMT + 5 pitfalls + 5 welding process implications.

ASME Section VIII Division 1 UCS-66 Toughness Requirements: Impact Testing Exemptions, Minimum Design Metal Temperature, and Welding Procedure Implications

ASME Section VIII Division 1 UCS-66 Toughness Requirements: Impact Testing Exemptions, Minimum Design Metal Temperature, and Welding Procedure Implications

ASME Section VIII Division 1 UCS-66 determines whether a carbon or low-alloy steel pressure vessel must undergo Charpy V-notch impact testing. 4 exemption curves (A-D), governing thickness, MDMT plot framework. 6 welding procedure implications (QW-403.6 / consumable / QW-409.1 heat input / preheat / PWHT / test plate). 9-step decision tree + 5 common UCS-66 pitfalls + Real Project SA-203 Gr E LNG vaporizer MDMT -73°C.

ASME Section IX QW-409.1 Heat Input Essential Variable: Welding Procedure Qualification Range Management for Pressure Vessel and Boiler Fabricators

ASME Section IX QW-409.1 Heat Input Essential Variable: Welding Procedure Qualification Range Management for Pressure Vessel and Boiler Fabricators

ASME Section IX QW-409.1 Heat Input Essential Variable — production heat input must stay within qualified range (typically +10% of PQR value). Heat input formula + 7 process efficiency factors + QW-403.6 supplementary impact testing + 5 procurement pitfalls.

ASME Section IX QW-403.4 Base Metal Thickness Range: P-Number Qualification Scope for Pressure Vessel and Boiler Fabricators

ASME Section IX QW-403.4 Base Metal Thickness Range: P-Number Qualification Scope for Pressure Vessel and Boiler Fabricators

ASME Section IX QW-403.4 Essential Variable — base metal thickness range qualified by single PQR test coupon per Table QW-451. P-Number qualification scope, 5 procurement pitfalls, multi-P-Number strategy.

ASME Section IX QW-462 vs QW-463: Welding Procedure Qualification Test Coupon Selection Guide for Plate and Pipe Welds

ASME Section IX QW-462 vs QW-463: Welding Procedure Qualification Test Coupon Selection Guide for Plate and Pipe Welds

Chapter-level guide to ASME Section IX QW-462 (specimen shape) vs QW-463 (specimen extraction location) for plate and pipe welds — 6 most-used QW-462 specimens, QW-463.1 plate / QW-463.2 pipe layouts, 5 procurement pitfalls.

WS D1.5 Bridge Welding Code: Welding Equipment Documentation Chain for Highway and Railway Bridge Fabricators

WS D1.5 Bridge Welding Code: Welding Equipment Documentation Chain for Highway and Railway Bridge Fabricators

How welding equipment supports fabricator AWS D1.5 bridge welding compliance — CVN toughness + tighter NDT + FCM provisions, AISC Steel Bridge Certification, 5 procurement pitfalls, dual D1.1 + D1.5 capability.

ATEX Directive 2014/34/EU: Welding Equipment Compliance for Hazardous Atmosphere Fabrication in Petrochemical, Offshore, and Hydrogen Service

ATEX Directive 2014/34/EU: Welding Equipment Compliance for Hazardous Atmosphere Fabrication in Petrochemical, Offshore, and Hydrogen Service

Why Wuxi ABK is the preferred welding equipment partner for ATEX-bound vessel fabrication — documentation depth aligned with Notified Body audit, PED Module H experience, calibration certificate focus, dual-cert (PED+ASME) experience.

ASME B31.4 and B31.8 Pipeline Transportation Welding Compliance: Documentation Chain for Oil and Gas Pipeline Fabricators

ASME B31.4 and B31.8 Pipeline Transportation Welding Compliance: Documentation Chain for Oil and Gas Pipeline Fabricators

How welding equipment supports B31.4 (liquid pipeline) and B31.8 (gas transmission) compliance — fabricator-held WPS, API 1104, ASME Section IX, 5 procurement pitfalls, spool prefab vs main-line laying.